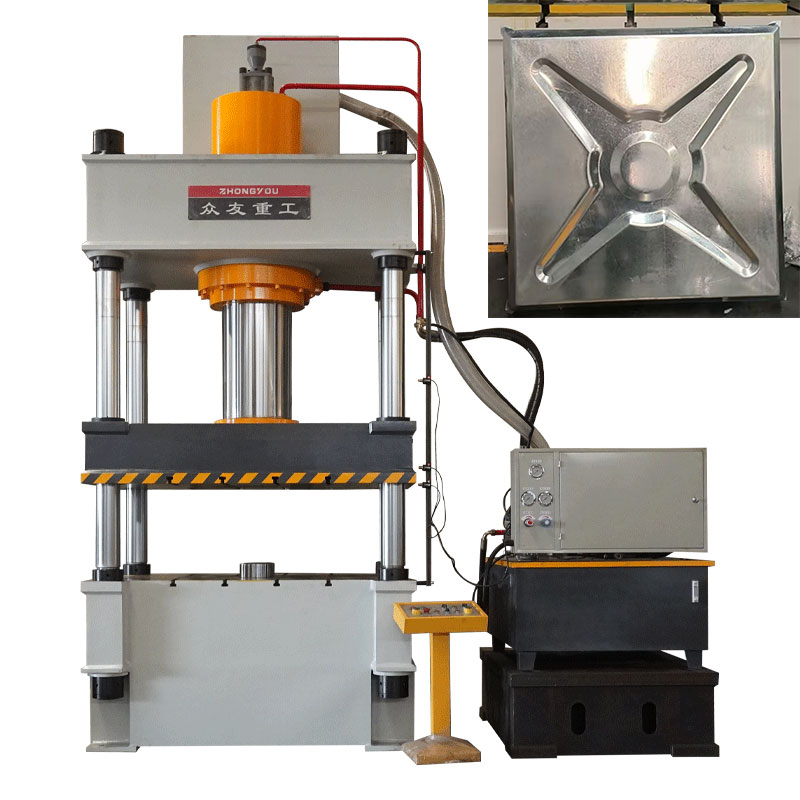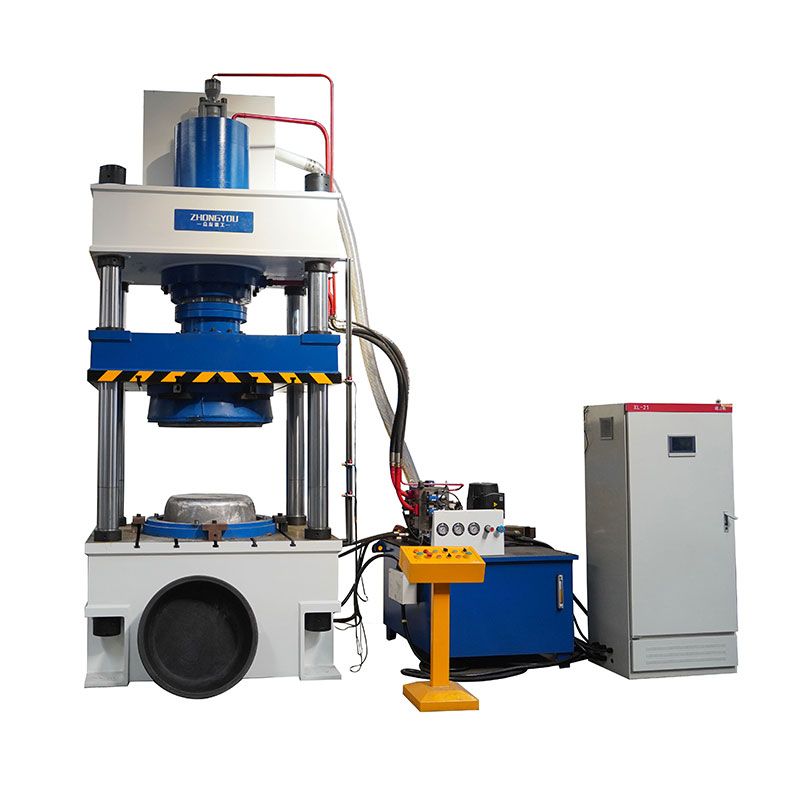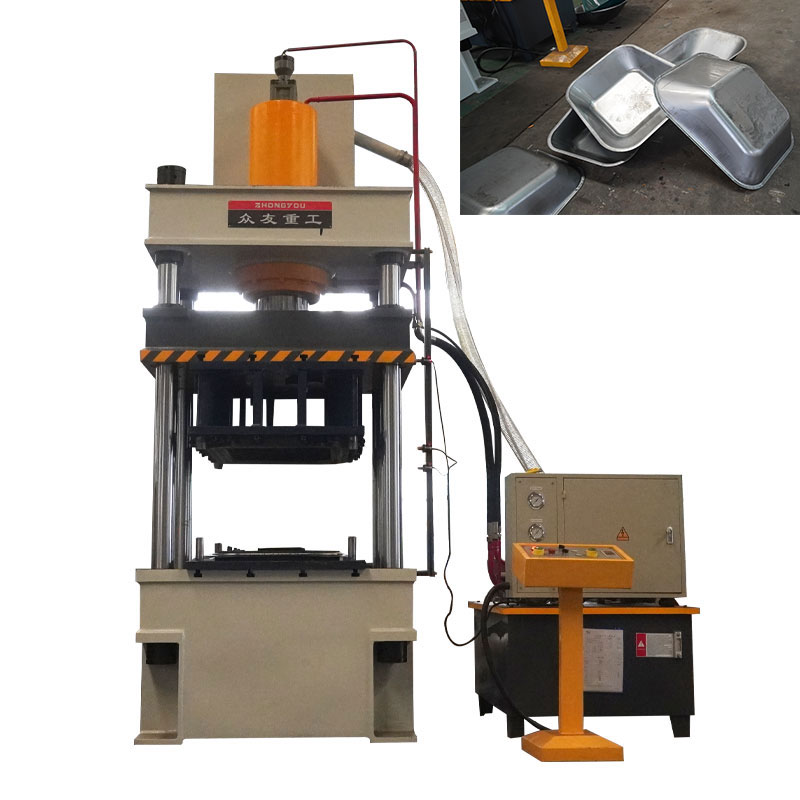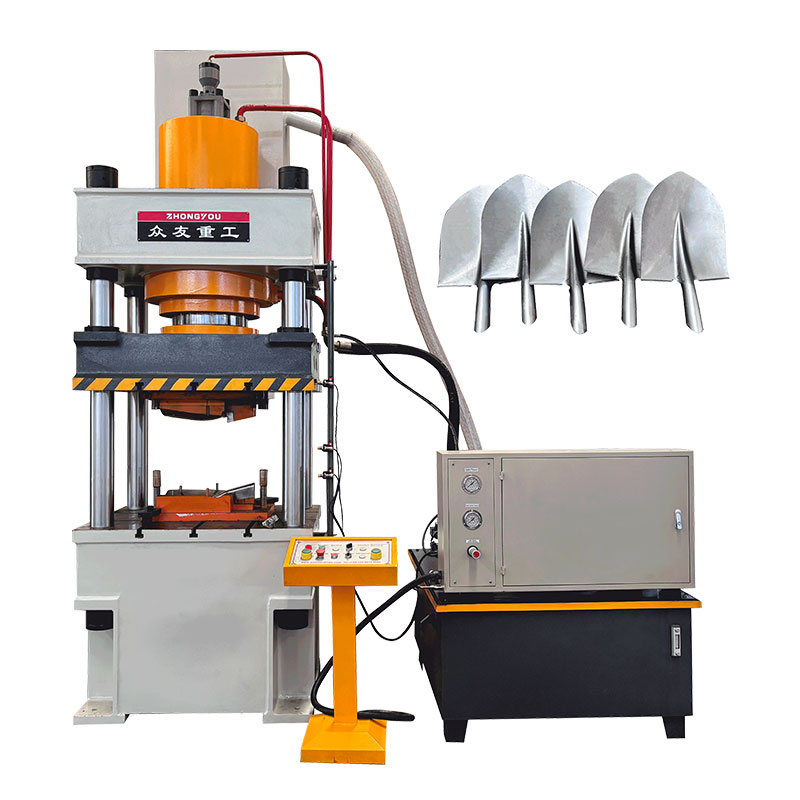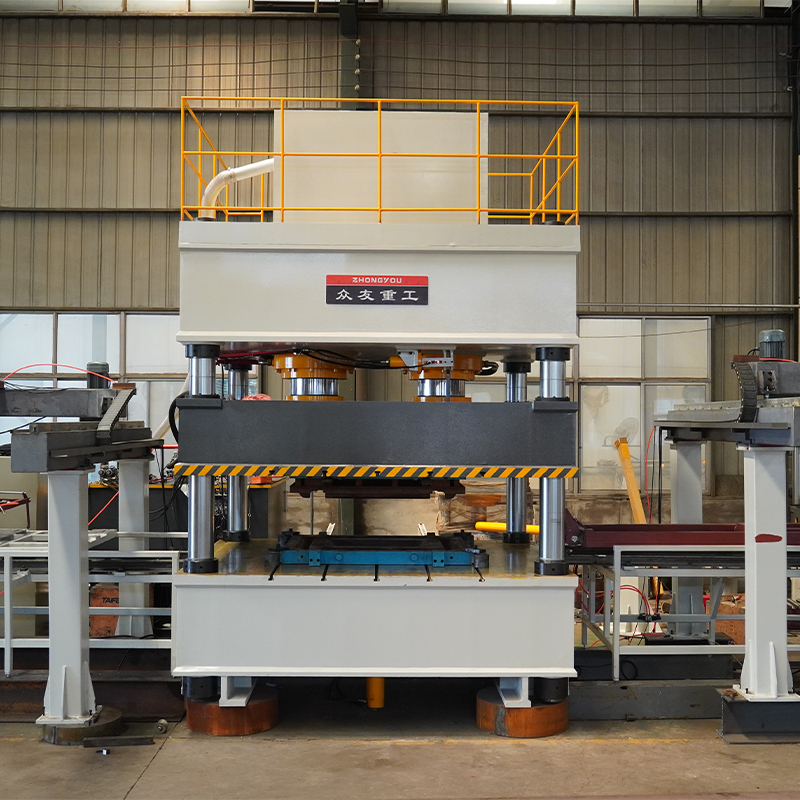
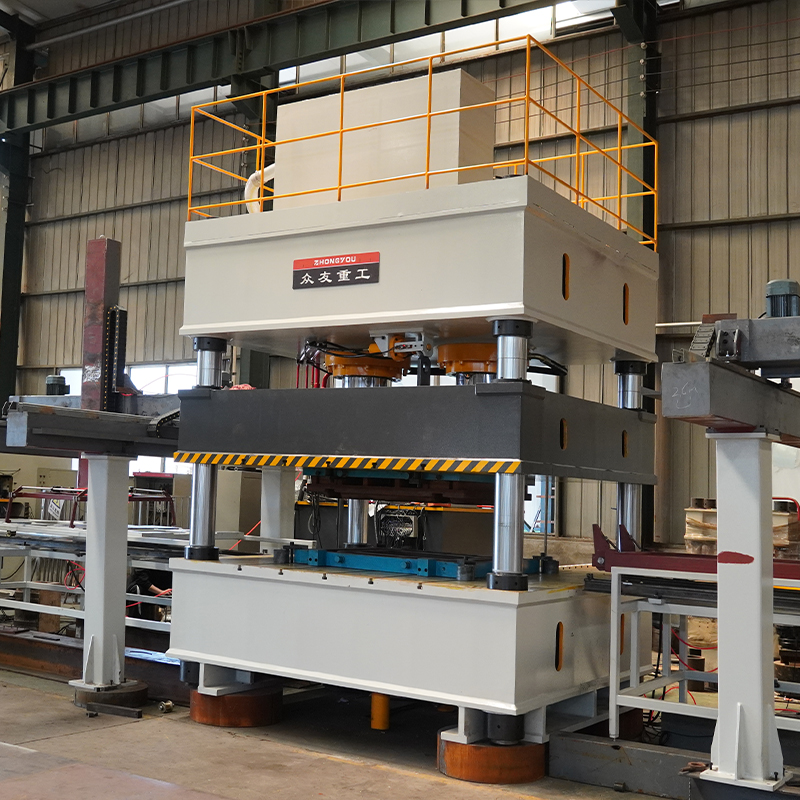
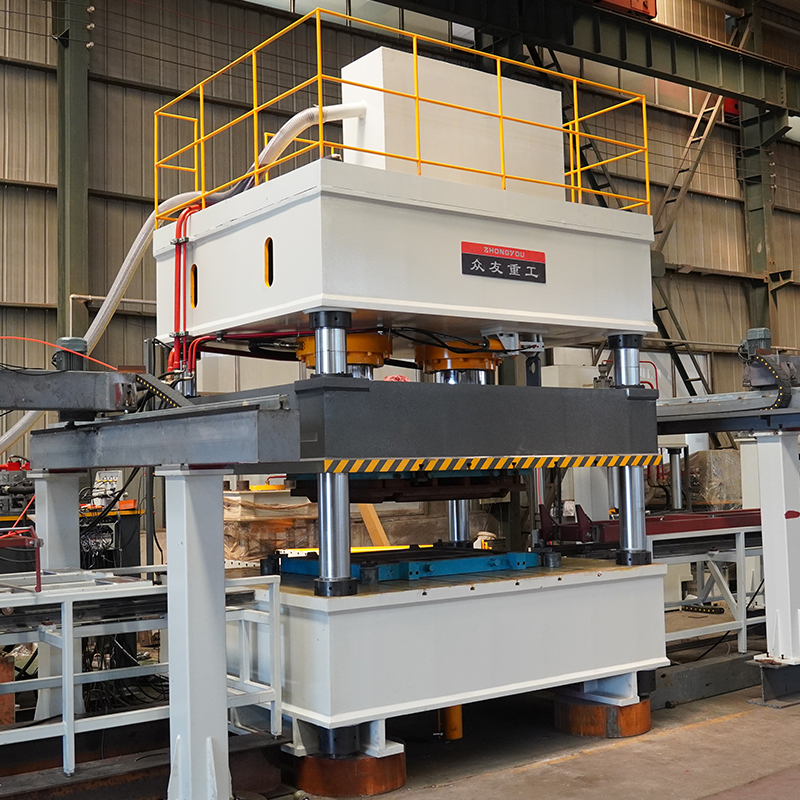
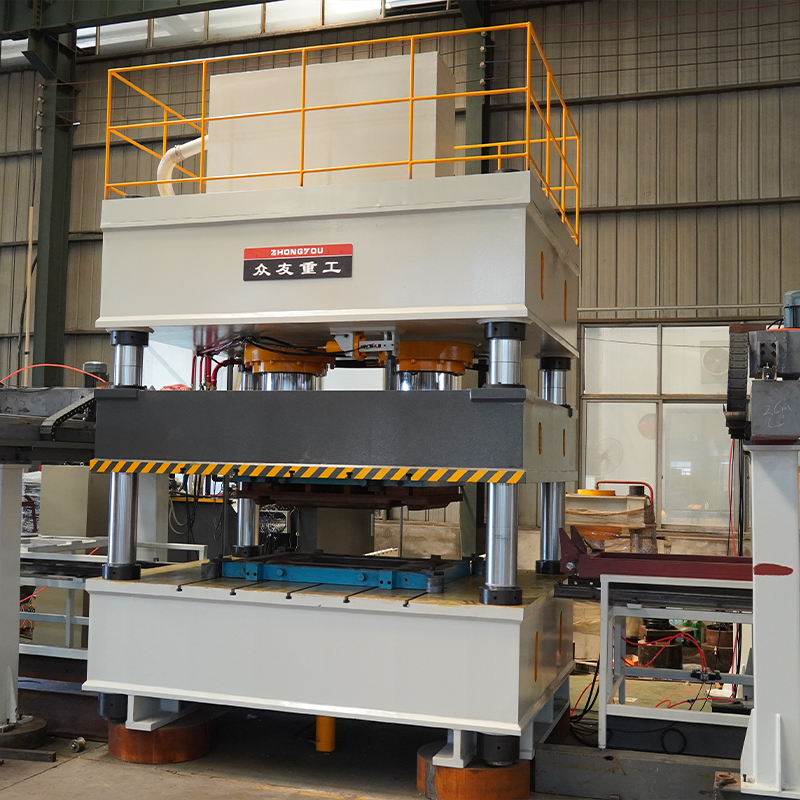
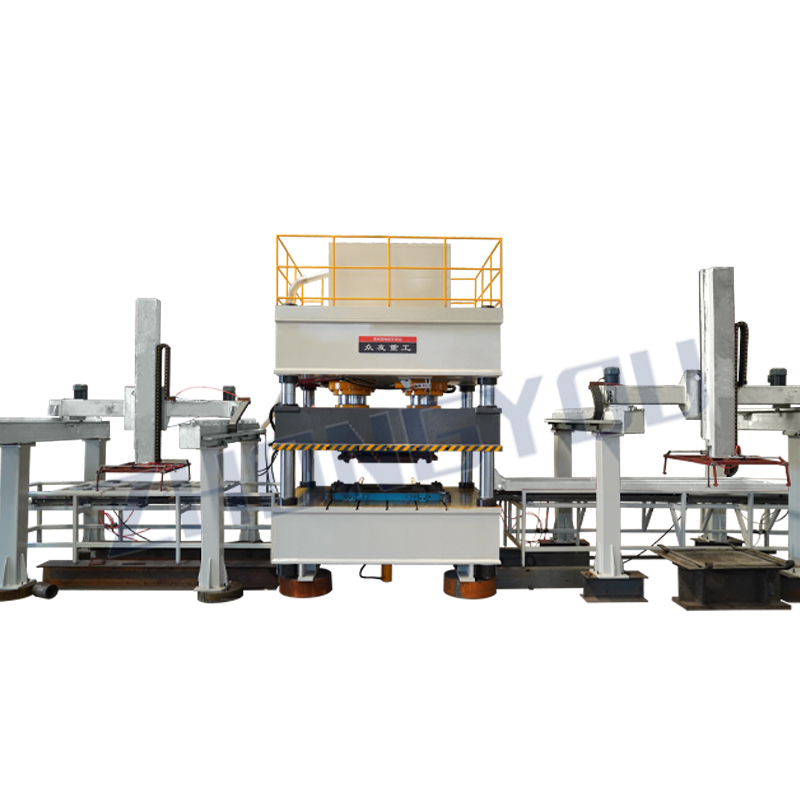
630-ton train door shaping production line hydraulic press steel plate correction press
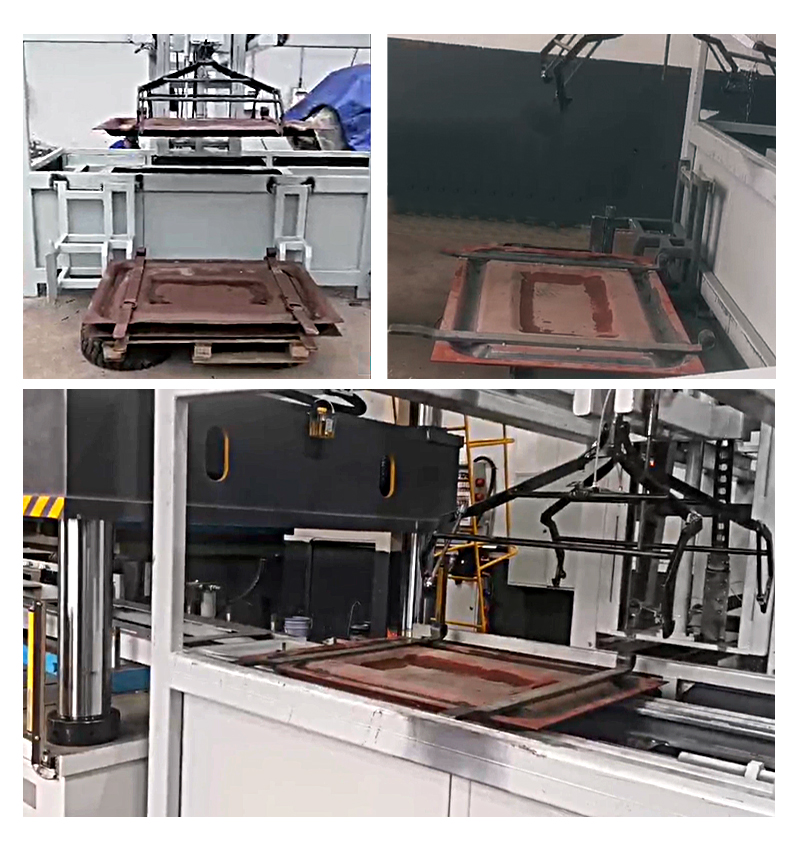
Shandong Zhongyou Heavy Industry Customers Customized a Train Door Panel Shaping Press for Inner Mongolia Customers, which is used to correct the deformation of the door panel of trains (including high-speed trains, high-speed trains, ordinary-speed trains, etc.) during manufacturing or maintenance. Its core function is to restore the design shape and dimensional accuracy of the deformed door panel by applying controllable pressure to ensure smooth door opening and closing, airtightness and appearance quality
Scan code plus WeChat
+86 13562463338

+86 13562463338
Video Show
Introduction of hydraulic press
The train door panel shaping press is used for correcting the deformation of the door panel of trains (including high-speed trains, high-speed trains, ordinary-speed trains, etc.) during manufacturing or maintenance. Its core function is to restore the design shape and dimensional accuracy of the deformed door panel by applying controllable pressure to ensure smooth door opening and closing, airtightness and appearance quality。
Core functions and application scenarios
Main function: correct the depression, bending and distortion of the door panel caused by stamping springback, transportation collision, long-term use or welding deformation (such as the deformation of the door frame and skin after assembly).
Application scenario: manufacturing process: after the door is stamped and formed, the shape deviation caused by the elastic recovery (springback) of the material needs to be corrected by a shaping press;
Maintenance link: in the depot or maintenance base, the door is deformed and repaired due to accidents (such as scratches), aging or fatigue;
Special requirements: for aluminum alloy, stainless steel and other lightweight materials of the door panel shaping (need to consider the material ductility and brittleness).
Structure composition
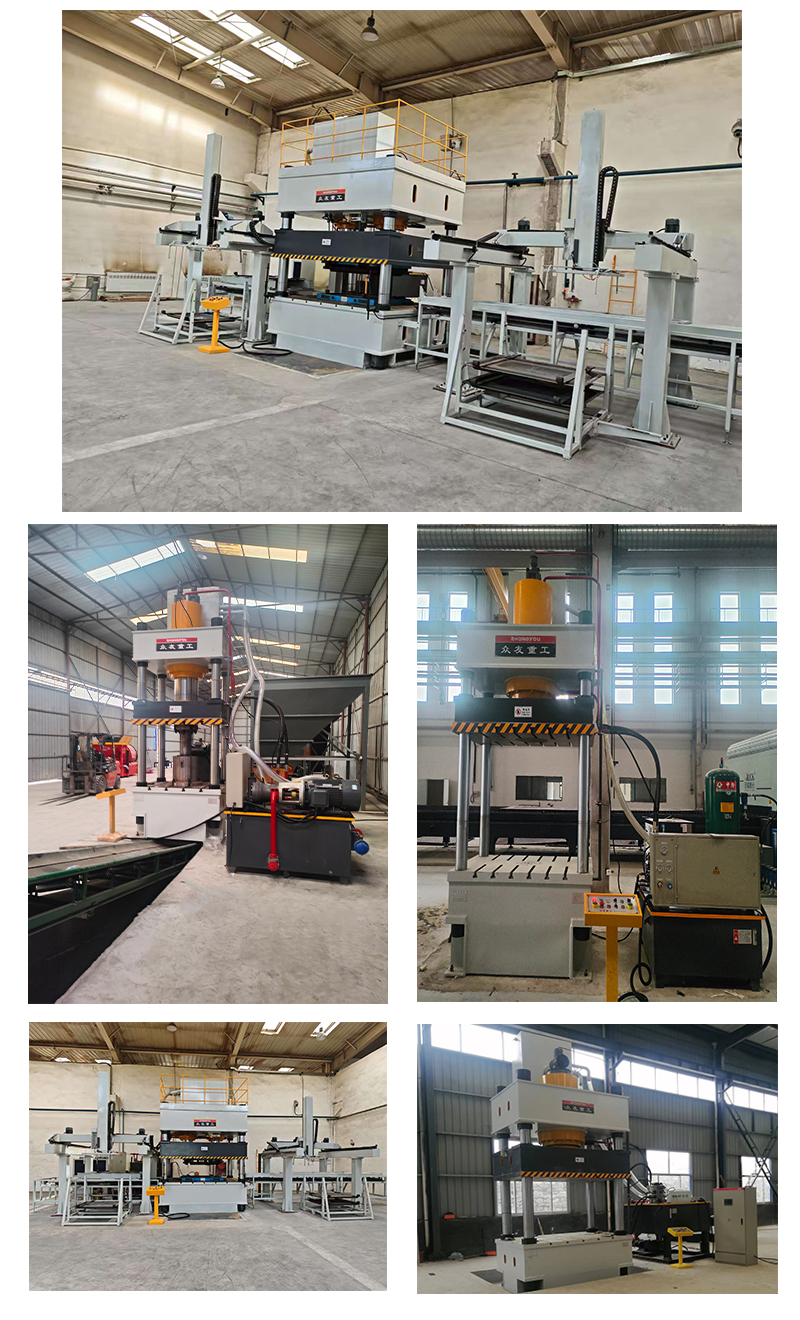
The train door panel shaping press usually consists of the following core parts:
1. Body (Rack)
Material: mostly high-strength steel plate welding or cast steel overall casting, need to have high rigidity and anti-deformation ability (to avoid the impact of the body's own deformation during pressure accuracy);
Structure: common frame type (such as C type, gantry type) or four-column type, for the slider (pressure head) to provide stable guidance, to ensure that the pressure is evenly applied to the door panel vertically.
2. Power and transmission system
Hydraulic drive (the most mainstream): through the hydraulic pump station to provide high-pressure oil, drive the hydraulic cylinder to push the slider down, the pressure range is large (up to hundreds to thousands of tons), suitable for large size, thick door plate shaping;
Mechanical drive (such as crank connecting rod type): The power is transmitted through the motor flywheel crankshaft, which is characterized by high speed and high precision, but the tonnage is relatively small (suitable for small and medium-sized door panels);
Servo drive (emerging technology): combined with servo motor and ball screw, can achieve precise pressure control (such as constant pressure shaping), energy saving and high degree of intelligence, but the cost is higher.
3. Mold system
Upper mold and lower mold: customized according to the shape of the door panel (such as rectangular, arc) and deformation area, usually replaceable modules (suitable for different models of door panels);
Positioning device: when the door panel is placed on the lower mold, it is fixed by positioning pins, clamps or pneumatic/electric clamping mechanisms to prevent displacement during the shaping process;
Auxiliary tools: Some equipment is equipped with heating devices (such as local induction heating) to soften high hardness materials (such as hardened steel) and reduce the difficulty of shaping.
4. Control system
Core components: PLC (programmable logic controller) touch screen human-machine interface (HMI), support pressure, stroke, speed of the precise setting;
Sensors: pressure sensor (real-time monitoring of output force), displacement sensor (monitoring of slider stroke), grating/laser range finder (detection of door panel deformation);
Safety protection: integrated emergency stop button, two-hand operation interlock, overload protection (to prevent overpressure damage to equipment or workpieces), in line with ISO 13849 and other safety standards.
GEO-CANARY-86EA1707
| YQ32 series three-beam four-column hydraulic press | |||||||
| project | 100T-A | 100T-B | 160T | 200T-A | 200T-B | 315T-A | 315T-B |
| Liquid pressure Mpa | 25 | 25 | 25 | 25 | 25 | 25 | 25 |
| Effective stroke of slider mm | 500 | 600 | 600 | 700 | 600 | 800 | 600 |
| Opening height mm | 800 | 900 | 900 | 1200 | 900 | 1250 | 1000 |
| Effective area of workbench | 630*550 | 750*700 | 660*600 | 1000*1000 | 800*800 | 1260*1160 | 800*800 |
| Idle descent speed mm/s | 100 | 100 | 100 | 100 | 100 | 120 | 120 |
| Pressing speed mm/s | 7-15 | 7-15 | 7-15 | 7-18 | 7-18 | 7-12 | 7-12 |
| Return speed mm/s | 90 | 90 | 90 | 90 | 90 | 100 | 90 |
| Motor power KW | 5.5 | 5.5 | 7.5 | 7.5 | 7.5 | 22 | 15 |
| Jacking force KN | 200 | 200 | 400 | 400 | 400 | 630 | 630 |
| Ejecting stroke mm | 200 | 200 | 200 | 200 | 200 | 300 | 300 |
| YQ32 series three-beam four-column hydraulic press | |||||||
| project | 400T | 500T | 630t | 800T | 1000T | 1250t | 1600t |
| Liquid pressure Mpa | 25 | 25 | 25 | 25 | 25 | 25 | 25 |
| Effective stroke of slider mm | 800 | 900 | 900 | 1000 | 900 | 900 | 1000 |
| Maximum opening height mm | 1250 | 1500 | 1500 | 1800 | 1600 | 1600 | 1800 |
| Effective area of workbench | 1260*1160 | 1400*1400 | 1600*1600 | 1500*1500 | 1500*1500 | 1800*1600 | 1600*1600 |
| Idle descent speed mm/s | 100 | 150 | 150 | 180 | 180 | 160 | 180 |
| Pressing speed mm/s | 5-11 | 10-18 | 9-18 | 9-18 | 10-18 | 10-18 | 6-14 |
| Return speed mm/s | 100 | 120 | 150 | 180 | 220 | 200 | 220 |
| Motor power KW | 45 | 45 | 45 | 37*2 | 37*2 | 37*2 | 37*2 |
| Jacking force KN | 630 | 1000 | 1000 | 1000 | 1000 | 1000 | 1600 |
| Ejecting stroke mm | 300 | 300 | 300 | 300 | 300 | 300 | 350 |
| YQ32 series three-beam four-column hydraulic press | |||||||
| project | 100T-A | 100T-B | 160T | 200T-A | 200T-B | 315T-A | 315T-B |
| Liquid pressure Mpa | 25 | 25 | 25 | 25 | 25 | 25 | 25 |
| Effective stroke of slider mm | 500 | 600 | 600 | 700 | 600 | 800 | 600 |
| Opening height mm | 800 | 900 | 900 | 1200 | 900 | 1250 | 1000 |
| Effective area of workbench | 630*550 | 750*700 | 660*600 | 1000*1000 | 800*800 | 1260*1160 | 800*800 |
| Idle descent speed mm/s | 100 | 100 | 100 | 100 | 100 | 120 | 120 |
| Pressing speed mm/s | 7-15 | 7-15 | 7-15 | 7-18 | 7-18 | 7-12 | 7-12 |
| Return speed mm/s | 90 | 90 | 90 | 90 | 90 | 100 | 90 |
| Motor power KW | 5.5 | 5.5 | 7.5 | 7.5 | 7.5 | 22 | 15 |
| Jacking force KN | 200 | 200 | 400 | 400 | 400 | 630 | 630 |
| Ejecting stroke mm | 200 | 200 | 200 | 200 | 200 | 300 | 300 |
| YQ32 series three-beam four-column hydraulic press | |||||||
| project | 400T | 500T | 630t | 800T | 1000T | 1250t | 1600t |
| Liquid pressure Mpa | 25 | 25 | 25 | 25 | 25 | 25 | 25 |
| Effective stroke of slider mm | 800 | 900 | 900 | 1000 | 900 | 900 | 1000 |
| Maximum opening height mm | 1250 | 1500 | 1500 | 1800 | 1600 | 1600 | 1800 |
| Effective area of workbench | 1260*1160 | 1400*1400 | 1600*1600 | 1500*1500 | 1500*1500 | 1800*1600 | 1600*1600 |
| Idle descent speed mm/s | 100 | 150 | 150 | 180 | 180 | 160 | 180 |
| Pressing speed mm/s | 5-11 | 10-18 | 9-18 | 9-18 | 10-18 | 10-18 | 6-14 |
| Return speed mm/s | 100 | 120 | 150 | 180 | 220 | 200 | 220 |
| Motor power KW | 45 | 45 | 45 | 37*2 | 37*2 | 37*2 | 37*2 |
| Jacking force KN | 630 | 1000 | 1000 | 1000 | 1000 | 1000 | 1600 |
| Ejecting stroke mm | 300 | 300 | 300 | 300 | 300 | 300 | 350 |